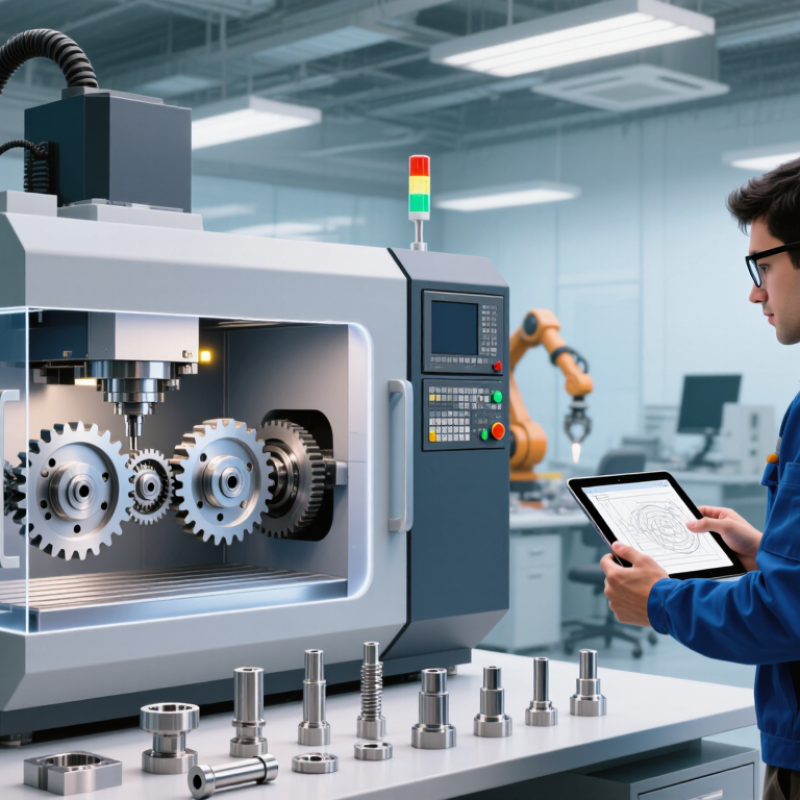
Choosing a CNC Milling Service in 2026 requires more than comparing hourly rates. A capable supplier should understand your material, tolerances, surface finish, and production volume. They should also explain limitations before accepting your order. That conversation often reveals more than a polished website.
Modern machining shops may use automated quoting, digital work instructions, five-axis equipment, and real-time production monitoring. These tools can improve consistency, but technology alone does not guarantee reliable parts. Ask how engineers review complex drawings, control tool wear, and inspect critical dimensions. Request measurable evidence, such as inspection reports, calibration records, material certificates, and representative sample parts. The details matter.
A dependable CNC Milling Service should communicate clearly from design review through delivery. Look for experience with your alloy, geometry, and required tolerances. Verify whether the supplier handles prototypes, low-volume batches, or repeat production without changing quality standards. Independent reviews and documented quality systems can support your assessment, but they are not perfect proof. No supplier is flawless. A missed assumption in your drawing can still create delays, even with an experienced team. Therefore, share complete files, realistic deadlines, and functional requirements early.
Price deserves careful attention. A cheap quote may exclude finishing, inspection, packaging, or expedited shipping. A higher quote may reflect better process control and lower long-term risk. Still, expensive does not always mean better. Compare capability, communication, quality evidence, lead time, and total cost together. This guide explores practical questions that help buyers make a confident, informed decision in 2026.
Before choosing a CNC milling service in 2026, define what your part must accomplish. Record the material, finished dimensions, tolerances, surface requirements, and expected quantity. A stainless-steel bracket needs different cutting conditions than an aluminum housing. Include a simple drawing, three-dimensional model, and critical measurement points. Experienced engineers will review these details before quoting. That review can reveal weak walls, difficult internal corners, or unnecessary tolerances.
Think about production reality, not only the first prototype. Ask how the service manages machine calibration, tool wear, inspection records, and material traceability. Confirm whether measurements use suitable equipment and whether inspection reports accompany the parts. Delivery timing also depends on programming, setup, finishing, and shipping. I have seen schedules fail because finishing was treated as an afterthought. That mistake is easy to repeat.
Tips: Mark only essential tolerances. Excessive precision raises cost without improving performance. Request a manufacturability review before production begins. Ask for a sample inspection report and clarify revision control. Keep communication written and specific. If your design is still changing, say so honestly. A reliable service should explain trade-offs instead of promising everything immediately. Some assumptions may be wrong. Test them with a small batch, measure the results, and revise the design when evidence demands it.
Material selection should follow the part’s actual load, temperature, and finishing requirements. Aluminum suits lightweight housings, while stainless steel handles corrosion and repeated cleaning. Engineering plastics can reduce friction, but they may creep under constant pressure. The 2024 World Materials Forum reported continuing volatility in metal costs, so request material certificates and confirm alloy availability before quoting. Ask whether the shop understands grain direction, heat treatment, and surface finishing. Small details matter.
Tolerance claims need context. A promised ±0.01 mm means little without datums, inspection temperature, and measurement uncertainty. ISO 2768 can guide general tolerances, but critical interfaces require a drawing-based tolerance scheme. NIST guidance stresses traceable measurement and documented uncertainty. I once treated every tight tolerance as automatically better. That increased cost without improving function. It was a useful mistake.
Review machining capability like a production engineer. Check five-axis access, maximum envelope, spindle speed, tool reach, and workholding options. Confirm whether the service performs in-process probing and final inspection. The ISO Survey 2023 recorded more than 1.2 million ISO 9001 certificates worldwide, yet certification alone does not prove milling competence. Request sample inspection reports, gauge details, and evidence from similar materials. Also ask about batch consistency. A perfect prototype can still hide unstable production performance.
Choosing a CNC milling service in 2026 requires more than comparing hourly rates. Ask what the equipment can actually hold during production. A modern three-axis mill may suit simple plates, while five-axis equipment reduces setups for angled features. Inspect spindle condition, work envelope, probe systems, and tool monitoring. Ask for recent tolerance data, not promises. A clean machine room helps, but it does not prove accuracy.
Technology should support repeatability, not decoration. Look for digital setup records, simulation before cutting, automated probing, and controlled revision histories. These tools can catch tool wear or a wrong offset before a batch is damaged. Request evidence from similar materials and geometries. Cutting aluminum is not the same as machining hardened steel. I once trusted a capability chart too quickly. The service had strong equipment, but weak documentation. That mistake cost time.
Quality control must be visible at each stage. Confirm incoming material certificates, in-process checks, first-article inspection, and final dimensional reports. Ask whether gauges and coordinate measuring equipment are calibrated on a defined schedule. Measurements should identify the part, operator, instrument, and revision. Also ask how nonconforming parts are isolated and corrected. No process is perfect. A reliable supplier explains failures without hiding them, then shows corrective action. Before approval, review a sample report and discuss a borderline dimension. That conversation often reveals more than a polished sales presentation.
A practical comparison framework for screening CNC milling suppliers without relying on company or brand names.
| Evaluation Dimension | What to Verify | Practical Benchmark for 2026 | Why It Matters | Priority |
|---|---|---|---|---|
| Machine Configuration | Number of controlled axes and simultaneous machining capability | 3-axis equipment is suitable for prismatic parts; 4-axis and 5-axis machining is preferable for complex geometries, undercuts, and reduced setup count. | More axes can reduce repositioning, setup error, and accumulated datum variation. | High |
| Work Envelope | Maximum X, Y, and Z travel, table size, part weight, and fixture clearance | The machine envelope should exceed the finished part size by approximately 20–30% in each relevant direction, while allowing tool access and workholding. | A nominally large machine may still be unsuitable if the tool, fixture, or rotary unit limits usable space. | High |
| Spindle Capability | Spindle speed, power, torque, taper, and cooling method | High-speed spindles support small tools and aluminum; higher torque and rigid tooling are more important for steel, stainless steel, and titanium. | Matching spindle characteristics to the material improves tool life, surface finish, and process stability. | High |
| Positioning Accuracy | Published accuracy and repeatability data, preferably measured under a recognized test method | Request documented machine-test results rather than relying only on a general specification. ISO 230-2 is a recognized reference for machine-tool positioning tests. | Repeatability and volumetric performance directly affect hole locations, mating features, and multi-face alignment. | High |
| Tolerance Capability | Ability to manufacture the drawing’s general and critical tolerances | For many standard milled parts, ±0. daw? Replace. Typical commercial capability is about ±0.10 mm; tighter tolerances such as ±0.025 mm require controlled processes, suitable machines, and inspection evidence. | Tolerance capability depends on material, feature size, geometry, thermal conditions, and measurement method—not only machine resolution. | High |
| CAM and Process Planning | CAM simulation, collision checking, toolpath optimization, and revision control | The supplier should be able to provide a documented process plan, simulate complex toolpaths, and maintain controlled revisions of CAD, CAM, and drawing files. | Digital process control reduces collisions, wrong-revision production, excessive tool engagement, and unnecessary cycle time. | High |
| Automation | Tool presetting, probing, pallet systems, bar-code or traveler control, and unattended machining controls | For repeat production, in-machine probing and tool-life monitoring are valuable. Automation should be supported by documented alarm handling and verification procedures. | Automation can improve repeatability and throughput, but it does not replace first-article inspection or process validation. | Medium–High |
| Material Control | Material identification, certificates, heat or lot traceability, and incoming inspection | Require material certificates when specified, including grade, heat or lot number, and relevant mechanical or chemical information. | Traceability helps prevent material substitution and supports investigation of dimensional or performance failures. | High |
| Workholding and Fixturing | Fixture design, datum strategy, soft jaws, modular tooling, and repeatable loading | The supplier should explain how datums are established and how thin walls, deep cavities, and distortion-prone parts are supported. | A strong machine cannot compensate for unstable workholding, incorrect datums, or excessive clamping force. | High |
| First-Article Inspection | Inspection plan, ballooned drawing, critical-feature records, and sample approval | For new or revised parts, require a first-article report covering all drawing characteristics or an agreed list of critical features before volume production. | First-article inspection confirms that the process can produce compliant parts before production quantities increase. | High |
| Measurement Equipment | Calibrated calipers, micrometers, height gauges, gauges, optical systems, and CMM access | Inspection equipment should be appropriate to the tolerance. Calibration records should be current and traceable to recognized national or international standards. | Measurement uncertainty must be sufficiently smaller than the tolerance being verified. | High |
| Quality Management | Documented procedures, nonconformance control, corrective action, and internal audits | ISO 9001 certification is a useful baseline for a documented quality management system, but certification should be supported by actual inspection and corrective-action records. | A quality certificate alone does not prove that every process or project will meet the required specification. | High |
| Geometric Dimensioning | Understanding and application of GD&T, datum schemes, position, profile, flatness, and runout | The supplier should interpret ASME Y14.5 or the applicable drawing standard consistently and identify ambiguous or conflicting requirements before machining. | Correct GD&T interpretation protects functional relationships that ordinary ± dimensions may not fully define. | High |
| Surface Finish | Ability to achieve specified roughness and cosmetic requirements | Common machined finishes are often specified using Ra values; confirm the measurement direction, inspection method, and whether secondary finishing is included. | Surface finish depends on tooling, feed rate, vibration, material, toolpath, and post-processing—not just the programmed step-over. | High |
| Process Validation | Capability studies, control plans, sampling frequency, and statistical monitoring | For repeat production, ask for evidence of process monitoring and agreed reaction plans for out-of-control or nonconforming conditions. | Validated processes reduce variation across batches and make quality performance more predictable. | High |
| Lead Time and Capacity | Quoted lead time, available machine hours, material procurement, and bottleneck operations | Request a schedule that separates engineering, material purchasing, machining, inspection, finishing, and shipping. Confirm capacity for repeat orders. | A low machining price is not useful if inspection, finishing, or constrained equipment creates schedule risk. | High |
| Finishing and Secondary Operations | Deburring, anodizing, plating, heat treatment, passivation, painting, and marking controls | Define the finishing specification, thickness or hardness requirement where applicable, appearance criteria, and certificate requirements before quotation. | Secondary operations can change dimensions, corrosion resistance, hardness, and cosmetic acceptance. | High |
| Documentation Package | Inspection report, material certificate, finishing certificate, deviation approval, and packing record | Agree on the required documentation before production. Records should identify the part revision, quantity inspected, results, and acceptance status. | Complete records simplify receiving inspection, audits, warranty investigations, and regulated-project compliance. | Medium–High |
| Communication and Engineering Support | Design-for-manufacturing feedback, response time, change management, and technical clarification | Prefer suppliers that identify inaccessible features, unrealistic tolerances, sharp internal corners, thin walls, and avoidable setups before production. | Early engineering feedback can reduce cost, lead time, scrap, and late drawing changes. | High |
| Supplier Qualification | Sample parts, references, audit access, equipment list, and documented performance history | Use a sample or pilot order to verify dimensional results, communication, packaging, documentation, and on-time delivery before approving larger volumes. | Actual evidence from a representative part is more reliable than a capability claim made without supporting records. | High |
Selection rule: Compare suppliers using the same drawing revision, material specification, tolerance requirements, inspection plan, finishing requirements, quantity, and delivery terms. The benchmarks above are general screening guidelines; final acceptance criteria should always be defined by the engineering drawing and purchase specification.
Choosing a CNC milling service in 2026 requires evidence, not polished promises. Ask for current ISO 9001 certification, scope, expiry date, and audit status. ISO’s latest Survey reports more than one million ISO 9001 certificates worldwide, but certification alone does not prove machining quality. For aerospace or medical work, verify relevant sector approvals and sample inspection records. Request a first-article report, material certificates, and measurement equipment calibration dates. Small details matter.
Lead time should appear as a dated production plan. Ask when programming, material purchasing, machining, inspection, and shipping will occur. Then test the answer with a small pilot order. Deloitte’s 2024 Smart Manufacturing Survey found that 86% of manufacturers expect smart manufacturing to drive competitiveness within three years. That pressure can improve scheduling, though digital dashboards can still hide overloaded machines. I have seen “five-day lead times” become three weeks after inspection queues were ignored.
Tips: Ask for weekly capacity figures, not vague statements. Confirm available machine hours, spindle size, tolerance capability, and backup equipment. Request the supplier’s on-time delivery rate for the previous six or twelve months. Compare promised capacity with your batch size, forecast, and peak-season demand. Also ask what happens when a machine fails. A credible answer includes a named recovery process, revised dates, and customer notification. Leave room for engineering changes; rigid schedules often fail there.
Choosing a CNC milling service in 2026 requires more than comparing the lowest quote. Price should reflect material, tolerances, setup time, inspection, finishing, and packaging. Ask for an itemized estimate. A cheap hourly rate may hide repeated setup charges or expensive rework. Request a sample inspection report and confirm how dimensional changes affect the final price. That small conversation can prevent a large invoice later.
Communication often reveals the real quality of a supplier. Can the engineer explain tool access, wall thickness, and surface-finish limits clearly? Do they ask useful questions before machining begins? Reliable communication includes written drawings, agreed revision numbers, response times, and progress updates. A shared photo of the first machined part can expose a problem before a full batch is produced. Silence is expensive.
Long-term support matters when designs change. Check whether the service can preserve inspection records, machining programs, and material certificates. Ask how they handle repeat orders, urgent revisions, and a failed part. Their answer should be practical, not vague. I have seen projects suffer because an early quotation was treated as permanent. It was not. Costs changed, and the missing assumptions caused friction. A better evaluation reviews three things together: transparent pricing, disciplined communication, and support that remains dependable after delivery.
This 2026 buyer scorecard compares the three factors most relevant when selecting a CNC milling service. Scores are normalized to a 100-point scale: pricing reflects cost competitiveness and quote transparency, communication reflects response speed and technical clarity, and long-term support reflects quality consistency, documentation, warranty coverage, and repeat-order capability.